A grain store is measured in tonnes, but a harvest arrives through time. That difference is easy to overlook when a new agricultural investment is announced. Empty space can accommodate a stock of grain; it cannot, by itself, sample a delivery, allocate a batch, remove moisture or release a lorry back to the field. The commercial value of the site depends on how those activities work together during the period when capacity is most urgently needed.
On 12 May 2025, Interfax reported Aterra's proposal for a grain-drying and storage complex in Krasnokholmsky district, Tver region, Russia. The announced system capacity was 30,000 tonnes. The report did not specify an investment amount or implementation timetable. It described a plan, not a commissioned operating result.
The proposal offers a starting point for a wider business question: what does a storage number tell a farm about its ability to receive a harvest? The answer requires a calendar, a description of the incoming grain and a map of the work between the field and the buyer. The analysis below sets out that decision framework; it is not an operating study of Aterra's facilities.
Keep stock capacity separate from processing flow
Storage capacity is a limit on the quantity held at a particular time. Processing capacity concerns movement through an operation over a period. A large store and a fast dryer answer different questions. Combining their headline figures without defining the connection can hide the very constraint an investment is supposed to remove. More space may help if finished grain has nowhere to go, but not if the immediate queue forms before conditioning.
A useful starting map follows an incoming load through reception, assessment, any necessary processing, allocation to storage and eventual dispatch. The actual arrangement can combine stages or use different routes for different grain. The point is not to impose a universal layout. It is to identify where a batch must wait, what resource releases it and whether that resource is shared with another activity.
Annual throughput is another distinct measure. The same storage space can handle more than one stock over a year if it is emptied and refilled. That does not demonstrate an ability to receive the same quantity in a short harvest window. A business case should therefore avoid using an annual movement figure as a substitute for the daily service that the farm requires at its busiest moment.
The arrival pattern matters more than an annual average
Averages can describe the scale of a business while concealing its busiest hours. Grain does not necessarily arrive at a constant rate, and a receiving plan should not assume that it does. Field activity, transport availability and decisions about which batches to move can concentrate deliveries. A timetable that works for an average day may fail when several loads need the same intake resource together.
The practical response is to construct several plausible arrival patterns rather than one smooth line. One pattern might concentrate arrivals into fewer working days; another might spread them out but require more handling per load. These are planning cases, not predictions of a particular harvest. Their value is to reveal which parts of the operation become limiting under different conditions and whether the proposed response is physically possible.
A queue also has consequences outside the site boundary. A vehicle waiting to unload is unavailable for its next journey. If dispatch from the field and reception at the store are managed separately, each team can appear efficient while the combined system loses time. Measuring the complete vehicle cycle makes that connection visible without assuming that every delay originates in the dryer.
Drying is a specification, not just a machine label
University of Minnesota Extension guidance distinguishes natural-air and low-temperature drying from high-temperature methods, explaining different timing, labour and quality considerations. It also discusses cooling after heated drying. These distinctions show why the word “dryer” alone is not a sufficient description of a handling system. The guidance is background, not an equipment specification for the Tver proposal.
For commercial planning, the important question is what service a supplier's performance statement actually covers. Does it describe a narrowly defined process under stated conditions, or the complete route to grain accepted for the intended destination? A purchaser needs the assumptions behind the rating before comparing offers. Otherwise two apparently similar capacities can represent different work, different input conditions or different boundaries of responsibility.
This is where technical assessment and the financial model must meet. The operating team should define the relevant crop, incoming condition and required output before the finance team assigns a unit cost. The article does not prescribe drying temperatures or storage thresholds. Those belong to qualified, crop-specific design and operating guidance. An economic comparison cannot safely replace that work with a convenient average.
Separate lots before counting free space
A facility can have spare volume without having the right space available for its next delivery. If batches must remain separate by ownership, intended use or agreed specification, capacity is divided into allocations rather than one interchangeable total. A partly occupied compartment may not be available for another lot. The amount of usable room therefore depends on the allocation plan as well as the physical dimensions.
Managers should describe the foreseeable lot structure before estimating utilisation. Which batches can share a destination? Which need dedicated space? What information must accompany a transfer? These questions help distinguish a genuine shortage of storage from a shortage of suitable compartments or an avoidable scheduling conflict. The solutions can differ: adding volume is not the same intervention as improving segregation or changing the sequence of movements.
Traceability has an economic purpose in this setting. When a batch changes location, the business needs to retain its identity and the basis on which it was accepted. That record supports later allocation and settlement. Without it, staff can spend time reconstructing what happened, while customers and owners disagree about which grain a result describes. Good records make physical capacity easier to use deliberately.
Buffer space buys time but does not create throughput
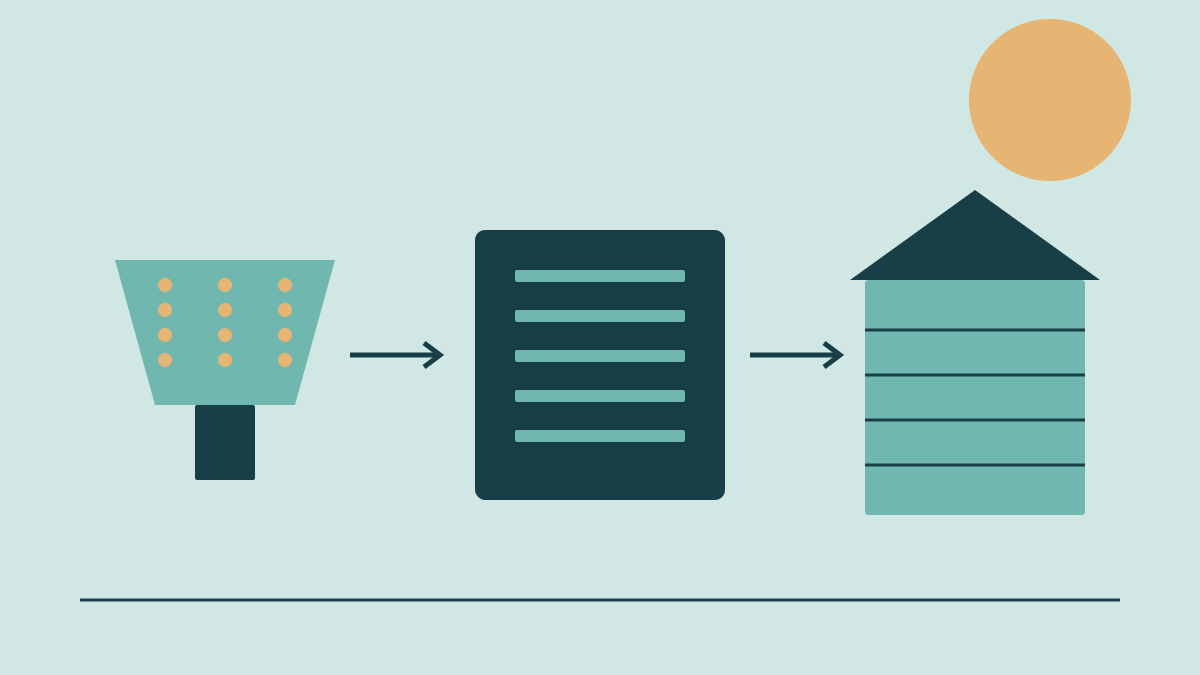
The sequence separates three functions without specifying a particular site's equipment, number of units or processing rate.
A buffer can absorb a temporary mismatch between arrivals and processing. It cannot remove a persistent mismatch without eventually filling. This is a basic scheduling distinction, but it has important investment consequences. A proposal that relies on additional holding space should state how and when that space will become available again, rather than counting the same room as an unlimited answer to every busy period.
The decision also needs a clear account of responsibility. Who authorises a load to enter a holding area, who monitors its condition and who decides its next destination? Those are operating questions with commercial consequences. The discussion is not an invitation to extend storage beyond suitable conditions. It is a reason to ensure that the proposed timetable respects the limits established by competent technical assessment.
Buffer policy should be connected to transport planning. If the site reaches its agreed limit, the response cannot be invented after more vehicles have already arrived. Advance arrangements might involve changing collection times or directing suitable deliveries to another approved route. Their feasibility depends on real access and agreements, not on drawing an extra box in a process diagram.
Follow costs across the whole route
The visible cost of drying is only part of the handling bill. Reception, testing, transfers, staff time, maintenance, storage management and dispatch can sit in different budgets. A narrow comparison may make one operation cheaper while shifting work elsewhere. A useful calculation identifies the boundary first: which activities are included, which are unchanged between alternatives and which arise only because of the proposed arrangement?
Mass and value also need consistent treatment. Incoming weight and the quantity accepted for a later sale need not be identical after processing. A business should record how its contracts handle those differences instead of describing every change in tonnes as a commercial loss or gain. The correct comparison follows the agreed product specification and settlement basis, not an unqualified total from the weighbridge.
Cost allocation should remain understandable to the people running the site. If every shared expense is loaded onto one process, a useful activity can appear uneconomic. If support costs are ignored, it can appear artificially cheap. Recording attributable work and explaining the treatment of shared resources gives management a clearer basis for comparison than a single unit-cost number without a definition.
Storage creates a timing option, not a guaranteed premium
Holding grain can separate the time of harvest from the time of sale. That flexibility may be useful, but its value is not established merely by having a building. Carrying costs, quality requirements, contractual commitments and available buyers affect what the business can actually do with the option. A later sale is a different decision from the investment in the facility that makes it possible.
The financial plan should therefore distinguish a handling benefit from an assumed price benefit. Reducing avoidable vehicle waiting or improving a dispatch process can be assessed through operating records. A hoped-for improvement in selling price depends on a later market outcome. Combining them into one optimistic return makes it difficult to see whether the project remains useful if that market assumption does not materialise.
This separation also improves accountability. The team responsible for operating equipment cannot control the whole commodity market. Equally, a favourable selling price does not prove that the handling system worked well. Evaluating operating performance and commercial timing separately allows the business to learn from each instead of letting one result conceal the other.
Dispatch is part of capacity planning
A store's ability to receive the next lot depends partly on its ability to release the previous one. Dispatch capacity, customer collection arrangements and transport schedules therefore belong in the receiving plan. A design focused only on intake can leave the business with grain ready to move but insufficient access to the equipment, staff or vehicles needed to complete the shipment.
Shared equipment deserves particular attention. If receiving and dispatch use the same handling resource, the timetable must account for both claims on it. The relevant test is whether the planned activities can coexist during their overlapping periods. Counting the full availability of the same resource twice produces capacity on paper that the operating team cannot deliver.
Maintenance and cleaning also need a place in that timetable. They should not be treated as exceptional interruptions simply because a calculation assumes continuous operation. The model should reserve the work that the equipment and procedures require, then test what remains available. That makes the stated service more credible and helps identify where an alternative route would be genuinely useful.
Compare complete alternatives
The choice need not be between doing everything on site and doing nothing. A farm might compare its own investment with an external service or a combination of the two. A fair comparison holds the required service constant: the same input assumptions, timing, acceptance basis and responsibility for transport. Without that consistency, an apparently cheaper offer may simply exclude an important part of the work.
External capacity also needs evidence. A nearby operator's advertised annual volume does not prove availability during the same harvest window. Access depends on booking terms, competing demand and the physical route. Conversely, owning equipment does not eliminate dependence on energy, spare parts or specialist support. Both arrangements have dependencies; the useful comparison makes them explicit.
A concise operating evidence set
Test handovers as well as equipment
An acceptance exercise can follow a representative lot across departmental boundaries. The test asks whether its identity, destination and readiness status remain clear when responsibility changes. A machine can perform its assigned task while the next team lacks the information or permission needed to proceed. Recording that handover exposes a problem that an isolated equipment demonstration may miss. The exercise should also ask how an exception is reported and who can decide a revised route. A documented answer gives staff something usable when the normal sequence cannot continue, rather than leaving them to interpret a capacity promise under pressure.
Before assigning a financial return to added capacity, management can establish a small set of records that links the harvest timetable to the site. The aim is not to collect every possible measurement. It is to identify where time and usable capacity are actually consumed.
- Arrival and departure times for loads, with the reason for material delays.
- Lot identity, acceptance basis and intended route through the facility.
- Processing availability under the conditions relevant to the work performed.
- Storage allocations and the dates on which space becomes available again.
- Shared-resource commitments for intake, dispatch and planned maintenance.
- Costs and settlement quantities measured across a consistent service boundary.
Together, these records turn an impressive storage figure into an assessable operating proposition. The unanswered question in any early announcement is not whether more space sounds useful. It is whether the planned system can provide the required service during the relevant season. A grain store earns its place in the business through that timetable, not through capacity alone.
Your perspective
Share your thoughts on the story.